Packaging Conveyor Systems
Belt, roller and modular conveyors that carry bottles, cartons, trays and packs between filling, coding, inspection and palletizing - matched to your line speed and layout.
Packaging Conveyor Increases Production
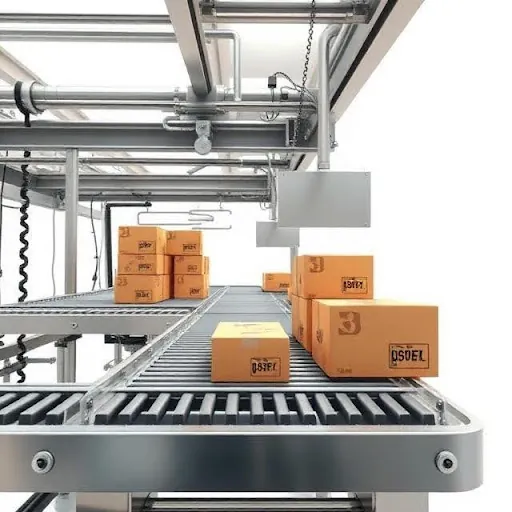
Packaging conveyor systems are designed to enhance material flow and streamline production lines in modern manufacturing and packaging environments. They enable efficient transportation of products such as bottles, cartons, trays, and packaged goods through key processes including filling, labelling, inspection, bundling and palletizing.
By integrating seamlessly with upstream and downstream equipment, packaging conveyors ensure a continuous, smooth product flow, reducing manual handling and improving overall workflow efficiency.
These systems are highly versatile and adaptable, capable of handling a wide range of product sizes, weights packaging materials, and line speeds while maintaining consistent accuracy. Built for durability and precision, packaging conveyors systems are well suited for industries such as food & beverage, pharmaceutical, FMCG and logistics, helping manufacturers achieve higher efficiency, product integrity, and improved operational productivity.
Where packaging conveyors run
Packaging conveyor systems are specified per station - filling, coding, inspection, case packing, palletizing.
Specifying a packaging conveyor
Common questions
What is the difference between a packaging conveyor and a general industrial conveyor?
What types of products can packaging conveyor systems handle?
Can packaging conveyors work with my existing machines?
What conveyor type is best for food packaging?
Does Welpack provide custom conveyor configurations?
Build the rest of the line
Machines that sit before or after this one on the line - each links to its own page.